


Closed die forging shapes heated metal inside matched dies, often through a blocker and finisher, before trimming. The die sequence controls fill and trim quality. This guide links that process to defects, records and buyer approval.

A shop-floor guide to die cavities, flash control and acceptance evidence.
What Is Closed Die Forging? A Buyer's Guide to Impression Die Forging
-
Home>
-
Blog>
-
Technology>
What Is Closed Die Forging? A Buyer's Guide to Impression Die Forging
08
2026.11
Forging Process Dossier
Read the die, not just the part outline.
Closed die forging is a controlled metal-flow process. The cavity, flash land, die sequence and acceptance plan all affect whether a drawing can be repeated in production.
Closed die forging shapes a heated metal billet between shaped dies, often in more than one impression, so the final cavity receives metal that has already been redistributed for filling and trimming.
A practical buyer question concerns the supplier's die route and process evidence. Can the supplier read the part geometry, propose a workable die sequence, control the variables that cause underfill or laps, and document the result? That answer sits in the tooling and process plan, before the first production batch.
HULK Metal produces custom hot die forged parts to the buyer's drawing. Production uses induction heating and multiple forging presses, inspection is carried out in-house, and heat treatment is handled by an audited partner. The public quality system is ISO 9001. Material, dimensions, inspection scope, MOQ and lead time require confirmation for the actual order.
What Closed Die Forging Means in a Press Shop
Impression die forging, also called closed die forging, forms metal inside a die impression that closely controls the finished geometry.
The upper and lower dies do not float around a simple ingot. They meet along a designed parting line and contain the reverse of the part shape. The heated billet is positioned in the lower impression, the press or hammer closes the tool, and metal flows into the cavity and into the flash allowance around the edge.
That distinction matters when a drawing moves from a prototype supplier to a production forge. A machined prototype can be cut from a solid block without deciding how metal will move. A closed die process must decide the billet volume, preform shape, blocker, finisher, flash control and trim line before the tool can be released.
Choose the perspective that matches your decision stage.
Engineering view
The process converts a finished-part drawing into a forging drawing, die layout and post-forging route. The review has to show where the parting line sits, which surfaces remain as-forged, where draft is needed, how much machining allowance is left, and which datums will be checked after forging or machining. The die sequence is part of the process definition, even when the purchase order only names the finished part.
Purchasing view
The quotation should make the scope visible. One supplier may quote forging only; another may include tooling, trimming, outsourced heat treatment, machining and inspection. Those offers are not comparable until the assumptions are written down. A low forging price can carry extra cost later if the die needs another trial, the machining allowance is wrong, or the inspection method was never agreed.
Capability view
Closed die forging covers many hot-forged industrial parts, but it does not make every geometry or material suitable. At HULK Metal the work is OEM production to the buyer's drawing, with no standard size catalogue. Open-die forging is not included in the current public capability list. Gears, shafts, aluminium forging, cold forging, rolled ring forging, forged wheels, titanium forging, H13 or D2 tool-steel forgings, and the restricted application sectors listed in the project capability file are not offered.
Engineering view selected.
A closed die forging page should answer three things in order: what the process physically does, where its failure points are, and what evidence a buyer can request before approving production.
The terminology also needs care. “Closed die” does not mean the dies form a perfectly sealed vessel. The tool has a controlled escape path for excess metal. That flash develops pressure in the final stage and helps the finisher fill before it cools and thickens. Trimming then removes the excess outside the intended part boundary.
Reading “closed” as controlled rather than sealed
For some buyers the closest familiar process is casting, because both use a shaped cavity. The comparison breaks down at the material condition. Casting fills a mould with liquid metal. Closed die forging deforms a solid heated billet. The process therefore has to manage billet volume, deformation direction, die closure, flash and trim, not only cavity filling and solidification.
The practical definition is therefore a production system rather than a single press stroke. It includes the die set, billet preparation, heating, one or more impressions, trimming, the specified post-forging route and the inspection plan. Remove any one of those controls and the word “closed die” says very little about the quality of the delivered batch.
A Die Set Is a Metal-Flow System, Not Just a Cavity
Useful details in a closed die set sit around the impression: the parting line, draft, corner radii, flash land and flash gutter.
The flow around the cavity
The impression creates the part shape, but the surrounding tooling determines how metal reaches the corners. A narrow flash land can restrict escape and raise pressure in the cavity. A wider or poorly matched land may let metal leave before thin sections fill. The balance is product-specific and belongs in die design and trial review, not in a generic tolerance promise.
This is why two parts with similar outlines can take different die routes. A shallow, open shape may fill from one impression. A part with a thin rib, deep pocket, stepped hub or long arm may need a blocker so the billet is redistributed before the finisher closes. The blocker has a production role: it creates a more suitable volume distribution for the final cavity.
Select a geometry condition to read the associated tooling concern.
1. Thin rib. Metal cools as it travels into a narrow section. The designer checks rib depth, width, radii and the amount of metal arriving from the blocker.
2. Deep pocket. A deep feature can create a dead zone or a lap. Draft and corner radii need to support removal and flow rather than merely suit the finished drawing.
3. Section change. A sudden thickness change can produce folding, uneven deformation or a difficult trim line. The transition may be redistributed before the finisher.
No geometry condition selected.
Draft matters for a simple reason: the forged part must leave the die. A finished-part drawing may show vertical walls because the part will later be machined or because the drawing was made without forging draft. The forging drawing has to account for release, unless the die designer can handle that surface another way. If this is not settled early, the tool may fit the nominal drawing but produce a part that cannot be ejected or trimmed cleanly.
Release, radii and trim are die decisions
Corner radii have a similar role. A sharp inside corner complicates die machining and can concentrate stress, restrict metal flow and shorten die life. Increasing a radius can change the finished shape, so the buyer's design authority has to agree where the change is acceptable. The forge should not quietly modify a load-bearing surface merely to make its own job easier.
Balancing release and useful shape
The flash system deserves the same review. Excess material must have somewhere to go, and the gap must close at the right moment. If the flash freezes too early, cavity pressure may rise beyond what the tool or press should carry. If it stays open too long, the thin sections may remain unfilled. The die designer works between those outcomes using the part geometry, material and production route.
A well-built die is therefore a sequence of decisions, not a copied cavity. The buyer does not need to specify every die feature, but the buyer should ask which features will differ from the finished-part drawing and why. That conversation is more useful than a blanket statement that a supplier can “hold tight tolerance”. The answer must be tied to specific surfaces, datums and operations.
Do not approve a die on a single successful trial forging. Check the whole trial batch for fill, trim quality, thickness distribution, surface condition and dimensional repeatability. A hand-picked sample can hide a process window that is too narrow for production.
From Billet to Finished Forging: The Sequence That Must Be Controlled
The production sequence succeeds only when each handoff preserves the assumptions made in die design.
Production normally starts with a billet cut to a planned volume. Too little metal leaves the finisher short; too much raises load, flash and trimming burden. The billet size is not judged by its nominal bar diameter alone. It has to match the part and the designed impressions.
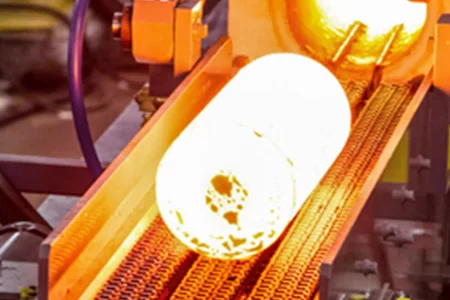
The billet is then heated to its forging condition. HULK Metal uses induction heating, which allows a short, repeatable heating step and can be integrated with the press line. The right temperature window is material-specific. A billet that is too cold raises resistance and may underfill; one that is overheated can increase scale, decarburization risk or grain-growth concerns. The exact window belongs to the approved process, not a generic article.
The route shown in the process sheet
No process step selected.
The blocker to finisher handoff is where many estimates go wrong. A simple part may run in fewer impressions; a complex part may need several. Each impression adds die work, tryout and process control. It can also reduce the load on the final cavity and improve metal distribution. The buyer should not assume that the lowest number of impressions is automatically the lowest total cost, because an unstable one-hit die can create more rework than a controlled multi-stage route.
Why the handoffs carry risk
Trimming follows forging. The trim die is matched to the forging geometry rather than a nominal drawing outline. Flash-line condition, trim burr and any distortion around the trimmed edge need to be checked. If trimming occurs at the wrong temperature, the edge can crack or tear. If the trim die is poorly matched, the part can bend or leave extra stock on a surface that later becomes functional.
Moving from trim to receiving condition
Heat treatment is a separate process step with its own evidence. At HULK Metal it is carried out by an audited partner. The buyer should know where the operation is performed, which process specification applies, how hardness or mechanical properties will be sampled, and how the parts are transferred and identified. “Heat treated” is not enough when the drawing calls for a named condition. The records should connect the delivered lot to the approved process.
Shot blasting, pickling or another cleaning step may follow heat treatment to remove scale or prepare the surface. Machining comes after the relevant thermal operation when the drawing requires dimensional recovery or critical mating surfaces. Inspection should cover the state that the customer will receive, not only the as-forged state. That is why a quoted process route must show where inspection occurs.
The factory question that prevents late surprises
In a factory review, the first question is how the route changes when the drawing is ambiguous. In our quotation review, the starting point is whether the file is a forging drawing or a finished-part drawing. If the parting line, draft, machining allowance, datum scheme or acceptance method are missing, the process cannot be quoted as though those choices were already settled. We raise them before die design, because a tool built on an assumption is expensive to correct.
Where Closed Die Forging Fails, and What the Evidence Looks Like
Most forging defects are not random surface flaws. Their position and repetition point back to a specific flow, temperature, tool or handling condition.
A defect name alone does not solve the problem. The useful inspection note says where it appears, whether it repeats on the same impression or die half, and whether it becomes clearer after trimming, blasting or machining. That evidence lets the forge change one cause instead of guessing at the whole process.
A review table connects the common failure modes in this article to process causes and visible evidence. It is a review aid, not an acceptance standard. The drawing or approved inspection plan decides what is acceptable for the order.
Table 1. Common closed die forging failure modes and the evidence that helps locate the cause.
| Defect | Usual mechanism | Where the evidence appears | First control question |
|---|---|---|---|
| Underfill or lack of fill | Metal cools or resists flow before a rib, corner or thin web fills | Same edge or pocket across parts; trim section may show missing volume | Is billet volume and blocker distribution adequate for this finisher? |
| Lap or fold | Metal folds over itself during preform or finishing | Curved seam near a radius, step or parting line; often opens after blasting | Does the die route direct metal into the feature instead of around it? |
| Cold shut | Two flow fronts meet after losing temperature | Faint seam at a junction or symmetrical flow front | Is the billet hot and fast enough through transfer and closing? |
| Flash-line crack | Stress concentration or poor trim condition at the flash line | Fine crack following the trimmed edge | Are trim temperature, die fit and edge condition under control? |
| Scale pit or rolled-in scale | Oxide is pressed into the surface during deformation | Random dark pits, especially where flow is heavy | Is heating, transfer time and scale removal matched to the route? |
| Decarburization | Surface carbon is lost during excessive heating exposure | Soft surface response; metallography confirms | Does the approved heating and sampling plan protect the required surface condition? |
| Mismatch or shift | Upper and lower dies are misaligned or the billet is placed off-centre | Repeating step at the parting line; uneven wall or stock | Are die alignment, guides and loading position checked? |
Underfill is a volume-and-flow question
The defect often looks like a rounded corner or a short rib, but adding pressure is not the only answer. The billet may be undersized, the blocker may send too little metal to that region, the corner radius may be too tight for the flow path, or the billet may arrive too cold. The pattern matters. A defect in the same pocket on every part points toward die design or volume. A defect that moves with heating delay points toward transfer and temperature.
Laps and cold shuts leave a seam with a history
A lap forms when metal folds over itself. It often sits near a radius, die step or parting line and may carry scale inside the fold. A cold shut is a flow-front seam: metal arrived from two directions after the fronts lost enough temperature to join cleanly. Both can look like a line after surface cleaning, so the investigation has to combine location, sectioning and process history. Grinding every mark without finding the cause risks leaving a deeper defect below the surface.
The trim line is part of the quality record
Flash-line condition should be inspected after trimming, not only before it. A crack that follows the trimmed edge can come from low trim temperature, a poor trim-die fit or a sharp geometry that concentrates stress. The buyer should know whether the edge is acceptable as-forged or will be removed by machining. Inspecting a coated or painted part is too late if the defect has already been hidden.
Mismatch repeats because the tool or loading repeats
A shift between die halves produces a step along the parting line and can leave uneven stock on one side. It may come from die alignment, guide wear, a worn insert or a billet placed off-centre. Measuring only the finished drawing can hide the cause because later machining removes some evidence. Record the as-forged condition and the die half on which the error repeats.
The same discipline applies to scale and decarburization. Both are surface effects, but they do not mean the same thing. Scale is oxide formed during heating and may be removed by blasting or pickling. Decarburization is a loss of carbon in the surface layer and can affect the response to heat treatment. A visual check may suggest a problem, but the required sampling and acceptance method come from the drawing or agreed specification.
Use pattern, location and process history together
No supplier can promise that a closed die process will never produce a crack or a lap. The honest control is a process plan with defined variables, a reaction plan when a pattern repeats, and evidence that suspect parts are contained. That is more useful to a buyer than a catalogue sentence claiming zero defects.
Part Geometry and Material Choice Change the Whole Cost Structure
Economically, closed die forging works when the drawing lets one tool repeat a stable shape; it becomes expensive when hidden features force trial, correction and extra operations.
What drives the die work
The first cost driver is not the outer envelope of the part. It is the combination of section changes, ribs, webs, bosses, pockets, draft, corners and surfaces that must remain as-forged. A part can look compact and still demand a difficult die sequence because the metal has to travel through narrow sections before the flash closes.
The second driver is the material. Carbon steel, alloy steel and stainless steel behave differently in heating, deformation and post-forging processing. A grade that is suitable for the application may still need a different die route or a more careful thermal plan. Material selection and material approval therefore belong in the same review as the forging drawing.
Select a geometry and material scenario to expose the review focus.
Compact, even section
A compact part with generous transitions may use a simpler route and fewer correction loops. The buyer should still confirm the parting line, draft, as-forged surfaces, machining allowance and trim condition. A simple shape can make a low-tooling estimate possible, but it does not remove the need to define the receiving inspection.
Thin ribs and deep pockets
Thin or deep features are flow problems. The die designer may add a blocker, change a transition or ask the buyer to relax a non-functional radius or wall condition. If the finished-part drawing treats every surface as final, there may be no room to add forging draft or machining stock. The right response is a drawing review, not a blanket promise that any feature can be forged.
Higher-alloy or stainless grade. These materials can increase deformation resistance, scale sensitivity and heat-treatment control requirements. The public HULK Metal approval list includes carbon steel, alloy steel and 304/316 stainless steel families, while the exact grade remains per drawing. The buyer should send the grade designation, equivalent standard and any restriction on substitutes. HULK Metal does not offer the restricted grades listed in the capability boundary or the restricted application markets.
No scenario selected.
A good drawing review asks which surfaces will remain as-forged and which will be machined. That decision controls allowance, datum selection and the sequence of inspection. If every surface is treated as final, the forge may have to leave stock everywhere, then the machine shop removes it. If too little stock is left, a normal forging variation can make the part unrecoverable.
Translate the finished shape into a forgeable shape
Draft is another place where the finished drawing can create false confidence. A vertical wall may be machined later, but it still needs a workable as-forged condition. Deep pockets and recessed flanges can require more draft than a shallow feature. The forge should mark where the as-forged shape will differ from the customer's final geometry. That is a technical proposal, not an unapproved design change.
Radii, transitions and impression count
Fillets and transitions affect both flow and tool life. A sharp inside corner can stop metal from reaching the bottom of a feature and can concentrate stress in the die. A larger radius can improve flow, but it may change the fit or load path of the finished part. The customer's design authority has to decide whether that radius is acceptable. A responsible forge does not hide that trade-off inside a die model.
Compare the received condition
The number of impression stages is a cost driver with a quality purpose. A second or third stage can improve distribution and reduce the load on the finisher, but it adds tooling and trial work. A single impression may be adequate for an open shape. The question is not “more stages are better” or “fewer stages are cheaper.” The question is which sequence produces a stable part within the agreed inspection scope.
Table 2. How drawing conditions change the review response.
| Drawing condition | Process response to review | Buyer decision |
|---|---|---|
| Thin rib or narrow web | Check blocker distribution, radii, flow distance and trim access | Relax a non-functional radius or accept a revised forging condition |
| Deep pocket or stepped hub | Review draft, flow dead zones and ejection | Confirm whether the as-forged wall can differ from the finished part |
| Critical machined bore or face | Plan allowance and the operation where the datum is created | State the finished requirement and inspection method |
| Higher-alloy or stainless grade | Review the approved material, heating route and outsourced heat treatment | Provide the grade, equivalents and property requirement |
Machining changes the cost comparison again. The near-net shape may reduce material removal, but critical bores, mating faces and tight fits often still require machining. A quote that says “forging only” and a quote that includes finishing are not alternatives unless the intermediate condition, allowance and acceptance criteria are the same. Buyers should compare the received part, not the process label alone.
Material availability can also change the route. A common carbon steel may be easier to source and forge than a more specialised alloy, but substituting a different grade without approval is not acceptable. The purchase order should state the required grade, any permitted equivalent and the evidence needed for the incoming lot. “Similar steel” is not a material specification.
Make the suitability answer conditional
When a buyer asks whether a part is suitable, the answer should be conditional and specific: the outer shape can be forged, but the thin rib needs a modified transition; the finished bore needs machining; the specified heat treatment will be outsourced; the acceptance method must be agreed. That kind of answer is more useful than an unconditional “yes” that leaves the difficult decisions for the first trial.
What the Drawing and Quality Records Must Tell the Buyer
A controlled drawing is the technical contract, but the inspection plan explains how that contract will be demonstrated.
A finished-part drawing describes the final component. A forging drawing describes the as-forged geometry, including parting line, draft, machining allowance, trim line and any as-forged dimensions. They are not interchangeable files. If only the finished-part drawing exists, the supplier needs a documented review and a customer approval path before the die is cut.
Datums matter because they determine how a dimension will be measured. A feature can be within a local size tolerance yet fail its position requirement when measured from the specified datum. The buyer should confirm which datums survive forging, which are established after machining, and whether the inspection report records the same setup used in production.
Select a record station to follow one lot through the release chain.
No record station selected.
Material records should be specific enough to show which grade was used. For incoming verification, HULK Metal can use in-house inspection resources such as composition, hardness, tensile and dimensional checks when the order requires them. The buyer should not assume a particular report format or third-party certificate. The public certificate statement is ISO 9001 only. If a buyer asks for a different certificate, that requirement must be discussed before order acceptance and cannot be invented by the supplier.
Process records should show the route actually approved for the part. That includes the number of impressions, the condition after trimming, the outsourced heat-treatment step and the point at which critical dimensions are measured. A record that says “forged and inspected” without identifying the operation or lot is too vague to support a corrective action.
Separate the inspection record from the route sheet
Inspection records should identify the drawing revision, the characteristics checked, the method used and the result. Sampling location and frequency are per drawing or agreed in the order. NDT, when required, should state the method and acceptance level specified by the buyer. A forge should not invent a UT, MT or PT level to make the quote look complete.
Dispatch records should connect the shipped quantity to the inspected lot and packaging. This step is especially consequential when parts receive outsourced heat treatment or when a batch is split between several operations. A clear lot identifier reduces the risk of mixing parts from different process histories.
Close the lot at dispatch
A compact document list for a closed die forging order often looks like this: the approved drawing revision; material grade and incoming evidence; the process or route sheet; heat-treatment records from the audited partner; dimensional and appearance results; any agreed mechanical or NDT records; and the packing list. The exact list depends on the product and order. The point is to agree it before production, not assemble a folder after a dispute.
The drawing may say `per drawing` for tolerances, allowances, hardness or sampling. That phrase is a valid production instruction only when the drawing or order also contains the corresponding requirement. If the requirement is missing, the supplier should raise it as a technical query.
How to Qualify a Supplier Before Tooling Is Cut
Supplier qualification is a review of evidence and ownership, not a tour of equipment names.
Check the boundary and the handoffs
Start with the parts the supplier can actually make. A forge may be capable in hot die forging but unsuitable for the proposed material, geometry, downstream finish or document pack. HULK Metal is an OEM supplier for custom hot die forged parts. The buyer's drawing is the starting point; there is no stock catalogue to match a part number against.
Ask who owns each step. Some operations may be in-house and others coordinated through partners. Heat treatment at HULK Metal is outsourced to an audited partner, so the buyer should ask how that partner is controlled, how parts are identified between sites and which records return with the lot. An outsourced step is not automatically a weakness, but an unclear handoff is a quality risk.
Use this pre-tooling review to decide whether the process is ready to quote.
No checklist item selected.
Separate the observation from the conclusion in the audit table. “The supplier has an induction line” is an observation. “The supplier can control the approved heating window for this grade through the shift” is a conclusion that needs evidence. The same distinction applies to inspection equipment: a hardness tester exists does not prove that the sampling position and acceptance rule are correct for the part.
Table 3. A practical supplier review for a custom closed die forging order.
| Review area | Acceptable evidence | Red flag | Why it matters |
|---|---|---|---|
| Drawing release | Approved forging drawing or controlled review notes | Supplier proceeds from an unchecked finished drawing | Die design decisions are being hidden in a price |
| Material | Grade and lot record with incoming verification | “Equivalent steel” stated without approval | Properties and processing can change with the grade |
| Die route | Impression sequence and trial acceptance criteria | One sample called production approval | Filling and trim stability are not demonstrated |
| Heat treatment | Named outsourced process, lot handoff and records | No owner for the outsourced transfer | Hardness and microstructure depend on the whole route |
| Inspection | Drawing revision, characteristics, method and result | Generic “QC passed” sheet | The buyer cannot trace a nonconformance |
| Change control | Written approval before die or process change | Correction made without customer notice | A small tooling change can move a critical feature |
| Dispatch | Lot, quantity and packing check | No link between inspected and shipped parts | Mixed lots can reach the assembly line |
The trial forging is the next gate. Agree what “successful” means before the trial: which surfaces will be checked, how the flash line will be judged, which dimensions are critical, whether sectioning is required and who signs the approval. A die that fills one visually good part is not yet a production route. The review should look for repeatability across the trial batch and the actions taken when a result misses the target.
Keep the commercial scope tied to the route
Commercial documents should follow the same logic. The tooling assumption, sample quantity, material grade, finishing scope, inspection scope and packaging method all affect price. If one supplier quotes a lower number because it leaves out an operation, the buyer needs to see that difference. A forge that explains the assumptions is easier to compare than one that compresses the scope into a single line.
Buyer Questions That Decide Whether Closed Die Forging Fits
Fitness depends on whether the geometry can be formed repeatably, the material and post-processing route are controlled, and the inspection evidence matches the application.
Use a decision sequence. First confirm that the part is inside the supplier's capability boundary. Then check whether the drawing can be converted into a stable die route. After that, compare the total delivered scope: material, forging, outsourced heat treatment, finishing, inspection, packaging and lead time. A process-name comparison without those conditions is too rough for a purchase decision.
Filter the buyer situations to see which review path applies.
Clear drawing and repeat demand
Move to a structured quote. Send the drawing revision, quantity, material, finishing requirement, inspection method, delivery basis and any packaging constraint. Ask the supplier to identify assumptions about draft, parting line, machining allowance and tooling. The commercial benefit of closed die forging depends on a process that can be repeated, not simply on a high first-run price or a low sample price.
Complex geometry or critical surface
Ask for a drawing review before tooling release. The reviewer should mark thin sections, deep pockets, sharp transitions, as-forged surfaces, machining datums and likely trim risks. If the finished drawing has no room for forging draft or machining stock, the design authority must decide how to resolve it. A sample request cannot replace that decision.
Outside stated capability. Stop the process comparison and return to the boundary list. Open-die forging is not a public HULK Metal capability. Gears and shafts, aluminium forging, cold forging, rolled ring forging, forged wheels, titanium forging, H13 or D2 tool-steel forgings, grade 4340 and the prohibited application sectors are not offered. A supplier review should not bury a capability mismatch under a generic “we can discuss” response.
No buyer situation selected.
A third question is whether the expected batch can absorb the die investment. Closed die work needs a die built for the part, so a one-off prototype and a repeat production program do not have the same economics. The exact tooling cost, MOQ and lead time are not public figures. They should be requested for the specific drawing and order scope.
Compare the delivered component
A fourth question is whether the buyer needs an as-forged part or a finished component. Closed die forging can create a near-net shape, but machining, heat treatment and surface protection may still be necessary. If the receiving drawing specifies a machined mating face, a hardness range or a surface treatment, those requirements must appear in the quote and route. Looking only at the forging operation understates the delivered cost and risk.
Test the supplier's response to uncertainty
A fifth question is how the supplier will handle uncertainty. A strong technical response identifies the assumptions, asks for the missing drawing information and describes what will be verified in the trial. A weak response promises that everything can be solved after the order is placed. The first approach creates a review trail; the second moves risk to the buyer.
Questions buyers ask before releasing a die
Is closed die forging the same as impression die forging?
Yes. The two names describe the same family of shaped-impression forging. The tool still has a controlled flash path, and that excess material is trimmed after forming.
Does every closed die forging need machining and heat treatment?
No single route fits every part. Some as-forged surfaces may be acceptable, while bores, seats, fits or surfaces altered by heat treatment may need machining. Heat treatment is specified from the material and service requirement. For HULK Metal orders it is carried out by an audited partner, and the hardness range, sampling position and records must come from the drawing or the agreed order requirement rather than a generic catalogue.
What information makes a closed die forging review useful?
Send the controlled drawing revision, annual or batch quantity, material grade, required heat-treatment condition, finishing scope, inspection method and delivery basis. State any constraint on draft, machining stock, as-forged surfaces, packaging or approved material equivalents. If the die sequence matters commercially, ask the supplier to identify whether a blocker, extra impression, trim tool or trial loop is included. Tolerances, allowances, hardness, sampling positions, MOQ, lead time and cost remain per drawing or confirmed for the specific order.
The final decision is not “closed die forging yes or no” in the abstract. It is whether this part, in this material, at this batch size, with this finishing route and this inspection scope, can be produced repeatably by the supplier being evaluated. Once that sentence is written down, the remaining questions are technical and commercial details rather than assumptions.
Boundary check before quotation
HULK Metal's position is narrow enough to be useful: custom hot die forged parts to the buyer's drawing, with induction heating, multiple forging presses, in-house inspection and outsourced heat treatment under ISO 9001. If the drawing contains a feature, material or application outside that boundary, the right next step is to stop and clarify the scope rather than force the part into a process description.
Base the decision on the controlled drawing, tooling route and acceptance evidence. A supplier's process name does not prove that this part can be filled, trimmed and documented repeatably.
Article Navigation
Others You Might Want to Know
Article Navigation
Industries
Foundries
More Closed Die and Hot Forging Articles from HULK Metal

Previous article: None
Next article: Induction Heating in Hot Die Forging: What It Changes in the Part